Tool length compensation
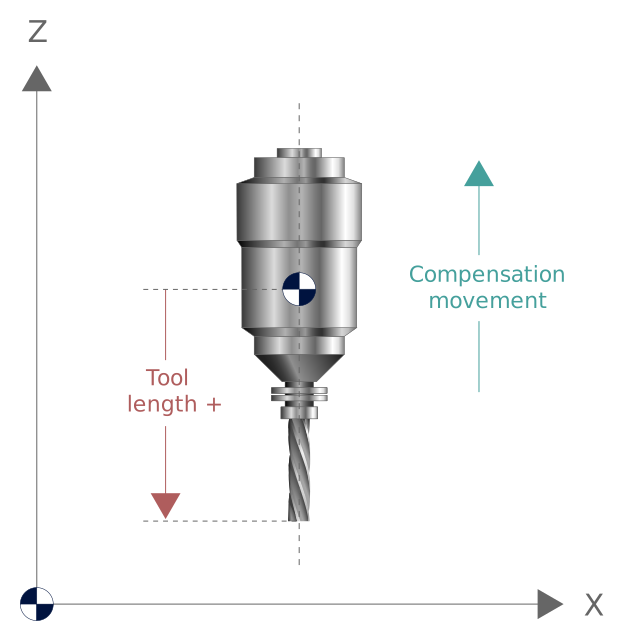
On Cartesian machines, tool length compensation (TLC) always acts in the direction of the 3rd main axis. With G17, this is generally the tool head axis.
If the tool is oriented in the negative direction to the Z axis, a compensating motion takes place to the positive direction of the Z axis.
Notice | |
If the mechanical machine structure defines a different tool head axis, the user must choose (G18, G19, #CS, #TRAFO) a suitable programming coordinate system (PCS) in order to calculate the tool length correctly. |
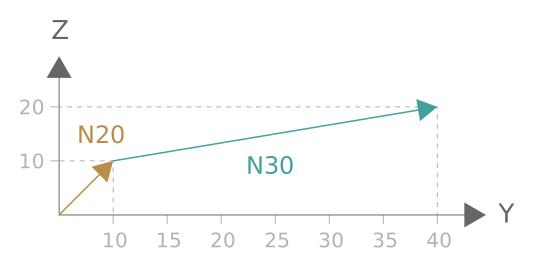
In the example below, tool length compensation is carried out in the Z direction. When the compensation data block D16 is selected in block N30, the compensation movement occurs in the Z direction jointly with the motion data block in N30.
Programming Example
N10 G01 F900 G17 ;X-Y plane, length compensation in Z+ (default))
N20 X150 Y10 Z10
N30 D16 Y40 Z15 ;Select length compensation D16. The
: ;compensation motion is executed.
:
N100 D20 ;Select tool compensation D20. The
: ;compensation motion only occurs with
: ;the next absolute motion block in the Z direction.
:
N200 G0 D0 X0 Y0 Z0 ;Deselect TLC
Compensation data block
D0: Length = 0 Radius = 0
D16: Length = 5 Radius = 5
D20: Length = 12.5 Radius = 5